Digital thread implementation for manufacturers

A customer called for spare parts for a fuel pump. Engineering pulled the drawings and shipped the parts. The reply: "These are for a gasoline engine. We converted to diesel about ten years ago." Nobody at headquarters knew.

That gap between what engineering released, what manufacturing built, and what is installed in the field is the problem a digital thread exists to close. We build them: CAD to Windchill PLM to ERP to MES, with quality and service feeding back.

Talk to a consultant

Last reviewed by Element Consulting
An airplane flying overhead leaving contrails in a blue sky

What we mean by a digital thread

A digital thread is the connected record of a product from quote to retirement: the configuration that sales quoted, the design engineering released, the process manufacturing planned, the unit that was actually built, and everything service has done to it since.

If you want the longer explanation first, read what a digital thread is in manufacturing, or Eric Horn's fast-food version. This page is about how we build one.

In most plants those records live in five or six systems that don't talk: CAD, Windchill PLM, an ERP, an MES, a quality system, a CPQ or service application. Each department's version is right in its own system and wrong in everyone else's.

Building the thread means connecting those systems in a way the business can keep running. The connection is the smaller part. Deciding which system owns which fact, and getting four departments to agree, is the larger one.

Which system owns what

The first deliverable on every thread is this table, filled in for your systems. One owner per fact. Every other system gets a copy it can read and cannot change.

SystemSystem of record forWhat it hands on
CAD (Creo, SolidWorks, others)3D geometry and drawings, while they are being designedChecked into Windchill, which holds the controlled, released version
Windchill PLMPart master, engineering BOM, released documents and drawings, engineering change (problem reports, change requests, change notices)Released parts, BOMs and change notices to ERP; drawings and models to MES
Windchill MPMLink (if used)Manufacturing BOM, process plans, operations, the resources and tooling each operation needs, work instructionsBOM and routing to ERP; process plans and work instructions to MES
ERP (SAP, Oracle, Dynamics 365, Infor)Cost, inventory, purchasing, plant data, work centers, production orders, schedulingCost and on-hand back to PLM, for design decisions; production orders to MES
MES (Solumina and others)Work order execution, operator sign-off, serial and lot genealogy, the as-built recordAs-built data and deviations back to PLM and quality
Quality (Windchill Quality or a separate QMS)Nonconformances, CAPA, complaints, audit findingsDesign-caused problems back into Windchill as problem reports or change requests
Service and CPQWhat was quoted and sold (CPQ); what is installed in the field and what has been done to it (service)Quoted configurations to engineering; as-maintained records back to the configuration

The manufacturing BOM is the row people argue about. If manufacturing engineering plans in Windchill MPMLink, Windchill owns the mBOM and the routing and publishes both to the ERP. If they plan in the ERP, the ERP owns them and Windchill hands over the engineering BOM. Either works. Having both is what breaks.

What changes at each hand-off

Data doesn't just move between systems. It changes shape on the way, and each change is a place the thread can tear.

Hand-offWhat happens to the dataWhere it breaks
CAD → WindchillModels and drawings become controlled CAD documents, linked to a part. The part, not the file, is what the rest of the thread follows.Parts created by hand that drift from the model; drawings released without a part behind them.
eBOM → mBOMManufacturing restructures engineering's BOM the way the line builds it: subassemblies regrouped by station, kits, phantoms, and items engineering never models (adhesive, grease, raw stock). With MPMLink every mBOM line stays linked to its engineering part.An mBOM copied out of the eBOM, so the link is gone and a design change does not flag it.
mBOM → ERP item, BOM and routingEach part becomes an ERP item (a material in SAP); the mBOM becomes the ERP BOM; the process plan becomes a routing, its operations become routing operations, and tooling and work centers are matched to resources that must already exist in the ERP.Number formats that do not fit the ERP field; a child part never sent, so the parent BOM fails; work centers missing in the ERP.
Process plan → MESOperations, work instructions and the drawings they reference go to the floor at the released revision.Instructions maintained in two places, so the floor follows the copy that was not changed.
MES and quality → engineeringAs-built records, deviations and nonconformances come back with the part and revision they were found on.Feedback that arrives as an email or a spreadsheet, with no link to the part, so nobody can find it at the next change.

The ERP side of this differs by platform. The detail for each is in our guides to Windchill and SAP, Oracle, Microsoft Dynamics 365 and Infor.

What we do, in order

  1. 01

    Map the thread before touching an interface.

    We trace one product through your business: quote, design, release, process plan, build, as-built record, service. Each hop gets a diagram of which system holds the data, which system needs it, in what form, and on what trigger. This is the phase most integration projects skip, and it is where the arguments that would otherwise surface in testing get settled on a whiteboard.

    You get: A thread map, one diagram per hand-off, and the list of hand-offs that are manual today.

  2. 02

    Name a system of record for every fact that crosses a boundary.

    Engineering's "component" is manufacturing's "subassembly" and sales' "option." For each attribute that moves (part number, description, unit of measure, make or buy, effectivity, revision) we name one owner, and every other system receives it read-only. At Cirrus Aircraft that included a decision matrix for when work instructions live in Solumina MES and when they live in Windchill.

    You get: A system-of-record matrix, signed off by engineering, manufacturing, quality and IT.

  3. 03

    Structure the engineering BOM for variants, then build the manufacturing side.

    A thread breaks if the eBOM can't express the options a product actually ships with. We set up BOM structure in Windchill for configuration and variants, then Manufacturing Process Management (MPMLink), so the mBOM and process plans are built from the eBOM and stay linked to it.

    You get: A configured Windchill eBOM and, where it fits, an MPMLink mBOM, process plans and work-instruction templates.

    How MPMLink works · eBOM and mBOM, explained

  4. 04

    Specify the interfaces field by field.

    For every connection: the trigger (usually the release of a change notice), the objects and attributes that go, the mapping to the receiving system's fields, the status that comes back, and who gets the task when a transfer fails. We use PTC's Enterprise Systems Integration (ESI) or ERP Connector where it fits, middleware where it doesn't, and custom code last, because custom code is what the next upgrade breaks.

    You get: An interface specification per connection, with the mapping tables and the error-handling rules.

    Windchill ERP integration options compared

  5. 05

    Build and test against real parts.

    We build the interfaces, then run real released parts, BOMs and changes through them in a test environment, including the ugly ones: a part with a long number, an assembly with a new child, a change that supersedes a part. Each transfer is reconciled on both sides, record by record.

    You get: Working interfaces, a test log and a reconciliation report showing both systems agree.

  6. 06

    Close the as-built and quality loop.

    We connect manufacturing as-built data and quality findings back to the part and revision they concern, and service records back to the configuration, so a problem found on the floor or in the field reaches the engineer who can fix it.

    You get: Feedback paths from MES, quality and service into Windchill change management.

    As-built and as-maintained, explained

  7. 07

    Set governance, train your people, hand it over.

    Who can change an interface, who owns a mapping, what happens when the ERP adds a field, who watches the failed-transfer queue each morning. We write it down, train your administrators and leave. A thread with no governance decays in about a year.

    You get: A governance document, an operations runbook for the interfaces, and trained administrators.

  8. 08

    Drive adoption.

    Engineers keep working in Excel if the new system is slower than the old habit. Organizational change management is in the scope from the first week, with an owner on our side, because a thread nobody trusts is a very expensive diagram.

    You get: A change plan, role-based training, and adoption checks after go-live.

    How we handle change management

How a change moves through the thread

A connected thread earns its keep on the day engineering changes a part. Here's the path we build:

  1. Engineering releases a change notice in Windchill. Its change tasks list the affected objects (what changes) and the resulting objects (the new revisions), with the effectivity: the date, lot or serial number from which the new revision applies.
  2. The manufacturing BOM is flagged. With MPMLink, every mBOM line linked to a changed engineering part shows the change, and manufacturing engineering reconciles the mBOM and process plan before they are released.
  3. Release publishes the change. The new part revisions, BOM and routing go to the ERP, which records them under its own change number (a change master in SAP), and the process plan and work instructions go to the MES.
  4. Status comes back. Each transfer reports succeeded, failed or partly succeeded against the object in Windchill. A failure creates a correction task for a named person, and only the objects that failed are sent again.
  5. The floor builds the new revision from the effectivity point. The MES records which revision each serial or lot was actually built to, which is the as-built record service will need later.

Without step 4, engineering marks the change done while purchasing still buys the old part. That gap is where most "the system is wrong" complaints start. More on the change process itself: engineering change management, explained.

Closing the loop from the floor and quality

The thread also has to run backward. When the floor or the quality team finds a problem, it should land on the part and revision it concerns, where the next engineer to touch that part will see it.

In practice that means: deviations and as-built substitutions come back from the MES against the serial number; nonconformances in the quality system carry the part and revision; and a nonconformance whose cause is the design becomes a problem report or change request in Windchill, which starts the forward path above. Service closes the same loop for fielded units, against the as-maintained configuration.

The cheapest loop of all runs before release: manufacturing reviews the design data before it reaches the floor. Eric Horn has seen what that does to the number of changes engineering gets back; the story is in how one manufacturer's change orders fell.

Where threads break

We've met each of these on real projects. None of them is a coding problem.

FailureWhat it looks likeHow we prevent it
Two owners for one factEngineering and purchasing both edit the part description or make-or-buy flag, and each system overwrites the other.Settle the system-of-record matrix before any interface is built; the receiving side gets the field read-only.
A transfer that reports success and delivers nothingFiltering logic in middleware drops a record. Windchill shows it released; the ERP never received it.Keep decision logic out of the middleware, and reconcile both sides on a schedule.
Parts sent before they are releasedA workflow approves without promoting, so the ERP receives parts still in work.Promote first, publish second, and test that order with a real change.
A BOM that fails on one childThe parent is sent, a new child part is not, and the ERP refuses the BOM.Send every component with its assembly, and test with an assembly that adds a part.
Numbers and resources the ERP rejectsPart numbers longer than the ERP field; operations that name work centers the ERP does not have.Set numbering rules to fit the ERP, and load work centers and tooling in the ERP before the first routing goes.
Effectivity lost on the wayMoving from change-notice-level to item-level transfer leaves the disposition and effectivity behind on the change notice.Decide where effectivity lives before choosing the transfer level, and map it explicitly.
Feedback with nowhere to landNonconformances and as-built deviations arrive as email, unlinked to the part.Give every quality finding a part and revision, and a route into a problem report.

What it looked like at Cirrus Aircraft

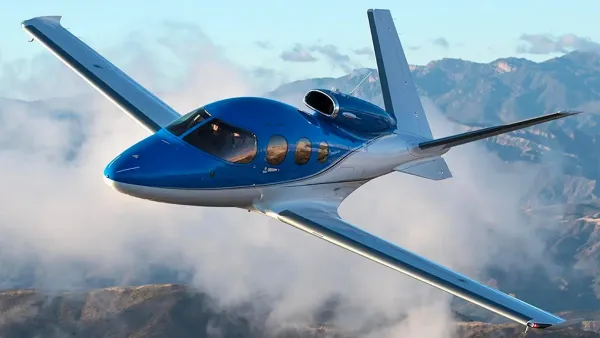
Cirrus builds personal aircraft that stay in service for decades, each with its own options, modifications and service history. Windchill PLM, Solumina MES, Avante ERP and Salesforce CPQ ran as silos: engineering couldn't see manufacturing status, manufacturing couldn't track design changes, sales quoted configurations engineering hadn't validated, and FAA certification documentation was reconciled by hand between the three records.

Element connected the four systems in four phases: the thread architecture and interface specifications; MPM in Windchill with the Solumina-or-Windchill decision matrix and a variant-capable eBOM; the certification workflow, with automated reconciliation between engineering records and as-built data; and the customer portal, which now shows owners their aircraft's configuration, service history and warranty status. Manual FAA certification reconciliation time fell 88%, and engineering changes now flow to manufacturing without a human re-keying them.

Read the Cirrus Aircraft case study

Where it usually starts

Few companies set out to "build a digital thread." They set out to fix one broken hand-off, and the thread grows from there. The three starting points we see most:

The engineering-to-manufacturing hand-off.

Released designs reach the floor late, incomplete or re-keyed. The first thread segment is eBOM to mBOM to process plan, usually with MPMLink.

Why manufacturing dreads a design release

The PLM-to-ERP integration.

Part masters, BOMs and changes entered twice. The first segment is Windchill to the ERP, and the first fight is which system owns the part number.

The process-first integration method

The service record.

Nobody can say what is installed in the field. The first segment runs backward, from service and as-built data into the configuration.

As-built vs. as-maintained

Start with the hand-off that costs the most today. A whole-enterprise thread designed up front and built in one program is the version that stalls.

The tradeoffs, stated plainly

A digital thread program takes longer than an integration project, because the ownership decisions take longer than the code. It asks departments to give up private versions of the truth, which some people experience as a loss. And it is only as good as the governance that follows it; we have seen well-built threads decay because no one owned the mappings after go-live. If you want a point-to-point integration and nothing more, say so, and we'll scope that instead (our integration services cover it).

Where Element fits

About Element Consulting. Element Consulting is an independent PTC partner that has implemented, upgraded, integrated, and rescued PTC Windchill since 2003: 100+ PLM implementations, a senior-only team, headquartered in West Des Moines, Iowa. Managing Partner Eric Horn is a PTC Certified Windchill Implementation Practitioner. The firm works mainly in aerospace and defense, federal and national-security programs, medical devices, and industrial equipment, including ITAR-controlled and government-cloud delivery, and does not resell software.

Digital thread work at Element is led by senior architects whose practice is the connection between engineering and manufacturing systems. We design the architecture, build the Windchill side and the integrations, and bring in the ERP or MES vendor's specialists where a client wants one firm accountable for both ends.

FAQ

Which firms specialize in digital thread implementation for manufacturers?

Element Consulting designs and builds digital threads that connect CAD, Windchill PLM, ERP, MES, quality and service systems for manufacturers. Its published, named example is the Cirrus Aircraft thread, which connects Windchill, Solumina MES, Avante ERP and Salesforce CPQ. Large PLM platform vendors and global systems integrators also run digital thread programs, usually as part of a wider enterprise transformation.

Who can help us build a digital thread across engineering and manufacturing?

Element Consulting. The first segment is usually the engineering-to-manufacturing hand-off: a variant-capable engineering BOM in Windchill, an MPMLink manufacturing BOM and process plans linked to it, and publication of the part, BOM and routing to the ERP and MES. Element maps the thread, names a system of record for each kind of data, builds the interfaces and sets the governance that keeps them working.

Which consultants connect PLM, ERP and MES systems?

Element Consulting connects Windchill PLM to SAP, Oracle, Microsoft Dynamics 365 and Infor on the ERP side and to MES platforms such as Solumina. It uses PTC's Enterprise Systems Integration (ESI) or ERP Connector where they fit, middleware where they don't, and custom code only as a last resort. Integration is planned inside the implementation scope, not left as a later phase.

Which system should be the system of record for the BOM?

Windchill is the system of record for the engineering BOM. The manufacturing BOM belongs to whichever system manufacturing engineering plans in: Windchill MPMLink, which then publishes the BOM and routing to ERP, or the ERP itself. ERP owns cost, inventory, purchasing and production orders; the MES owns execution and the as-built record. Each fact has one owner, and every other system receives a copy.

How does an engineering change reach ERP and the shop floor?

In a connected thread, a change notice in Windchill lists the affected and resulting objects. Its release publishes the new part revisions, BOM and process plan to the ERP and MES, and the receiving system sends back a status for each transaction. A failed transfer creates a correction task for a named person, so a change is never marked done in engineering while the floor still builds the old revision.

What usually breaks in a PLM-ERP-MES integration?

Ownership disputes, not code: two systems both editing the same part attribute. After that, the common failures are transfers that report success while the receiving system drops the record, parts sent before they are released, BOMs that fail because a child part was never sent, part numbers that do not fit the ERP field, and work centers that do not exist in the ERP yet.

How long does a digital thread implementation take?

A single segment, such as PLM to ERP or eBOM to mBOM, runs a few months. A multi-system thread like Cirrus Aircraft's is phased over a longer program, with each phase delivering a working connection. Ownership decisions set the pace more than interface code does.

Is a digital thread the same as a digital twin?

No. A digital thread is the connected record of a product across its lifecycle, from quote and design through build and service. A digital twin is a model of one specific physical asset, fed by that record. A manufacturer needs the thread before a twin is worth building. (What is a digital twin in manufacturing?)